Material Preparation, Diameter Control and Downstream Handling for PU / TPU
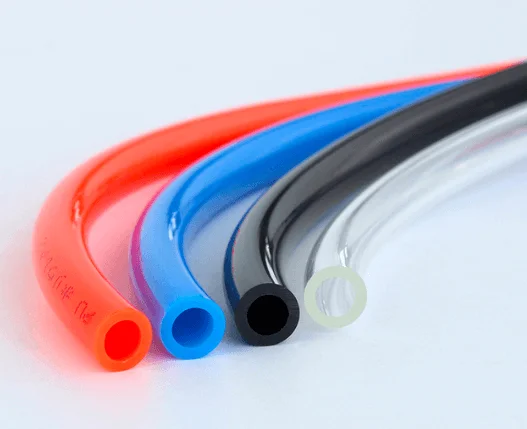
PU and TPU are flexible polyurethane materials, and their extrusion behavior is different from rigid pipe materials. Before selecting machine size, confirm the compound grade, hardness and finished tube use; the common plastics used in extrusion guide explains why TPU tubing needs a different process route from rigid PVC, PE or PP products.
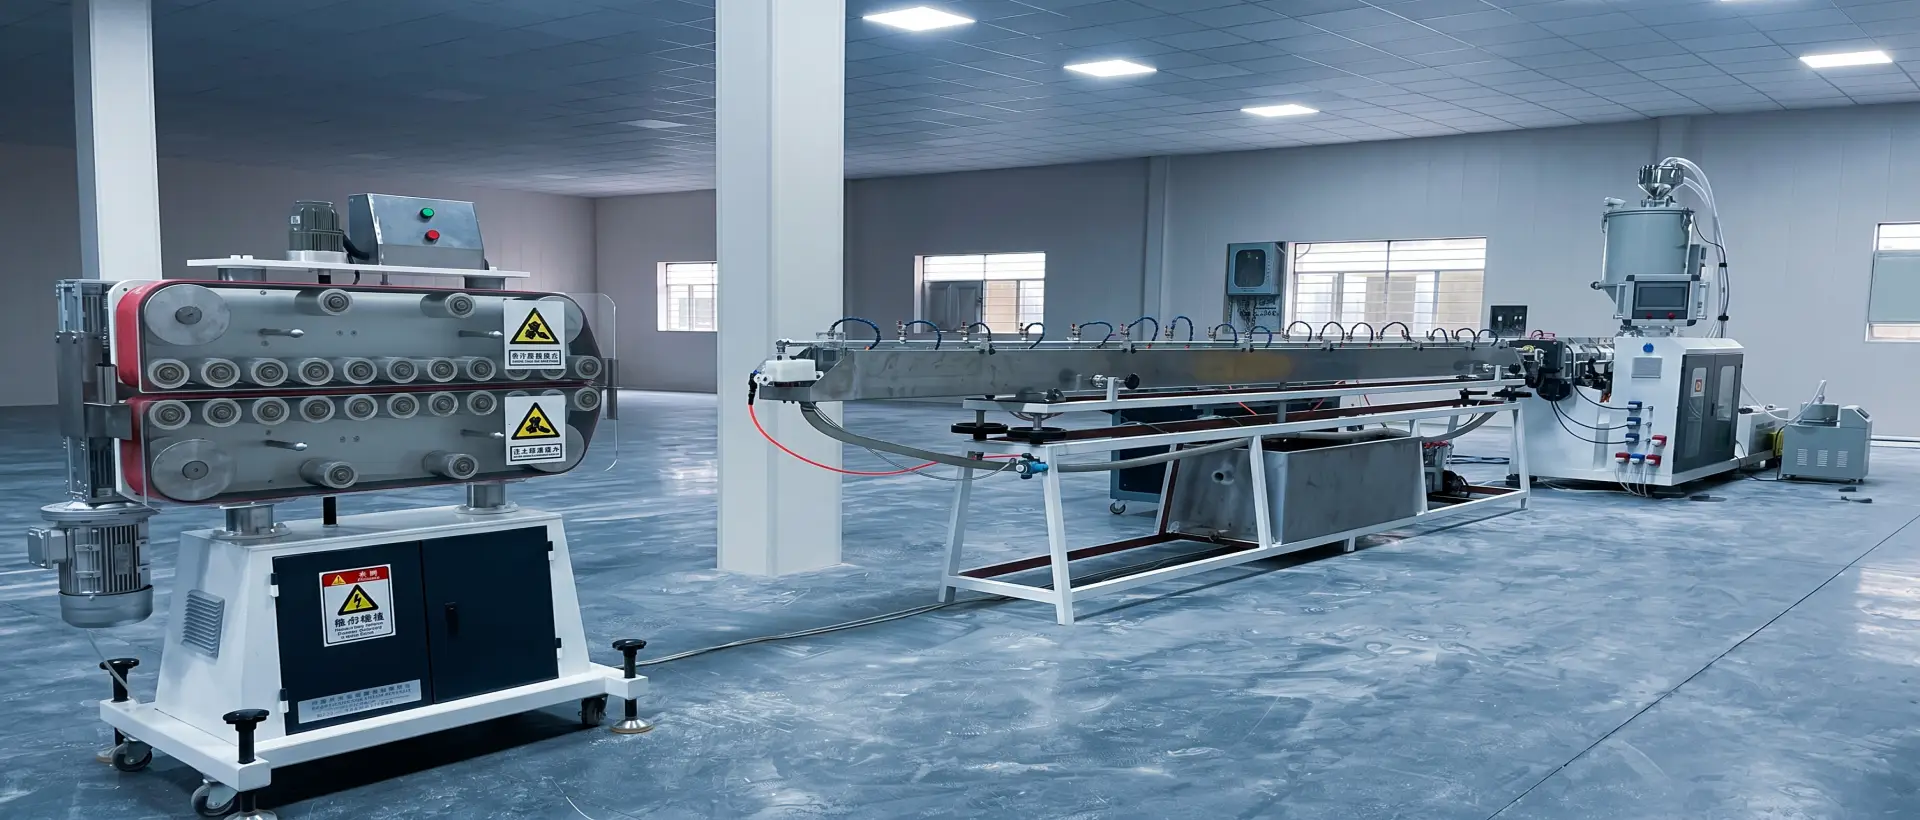
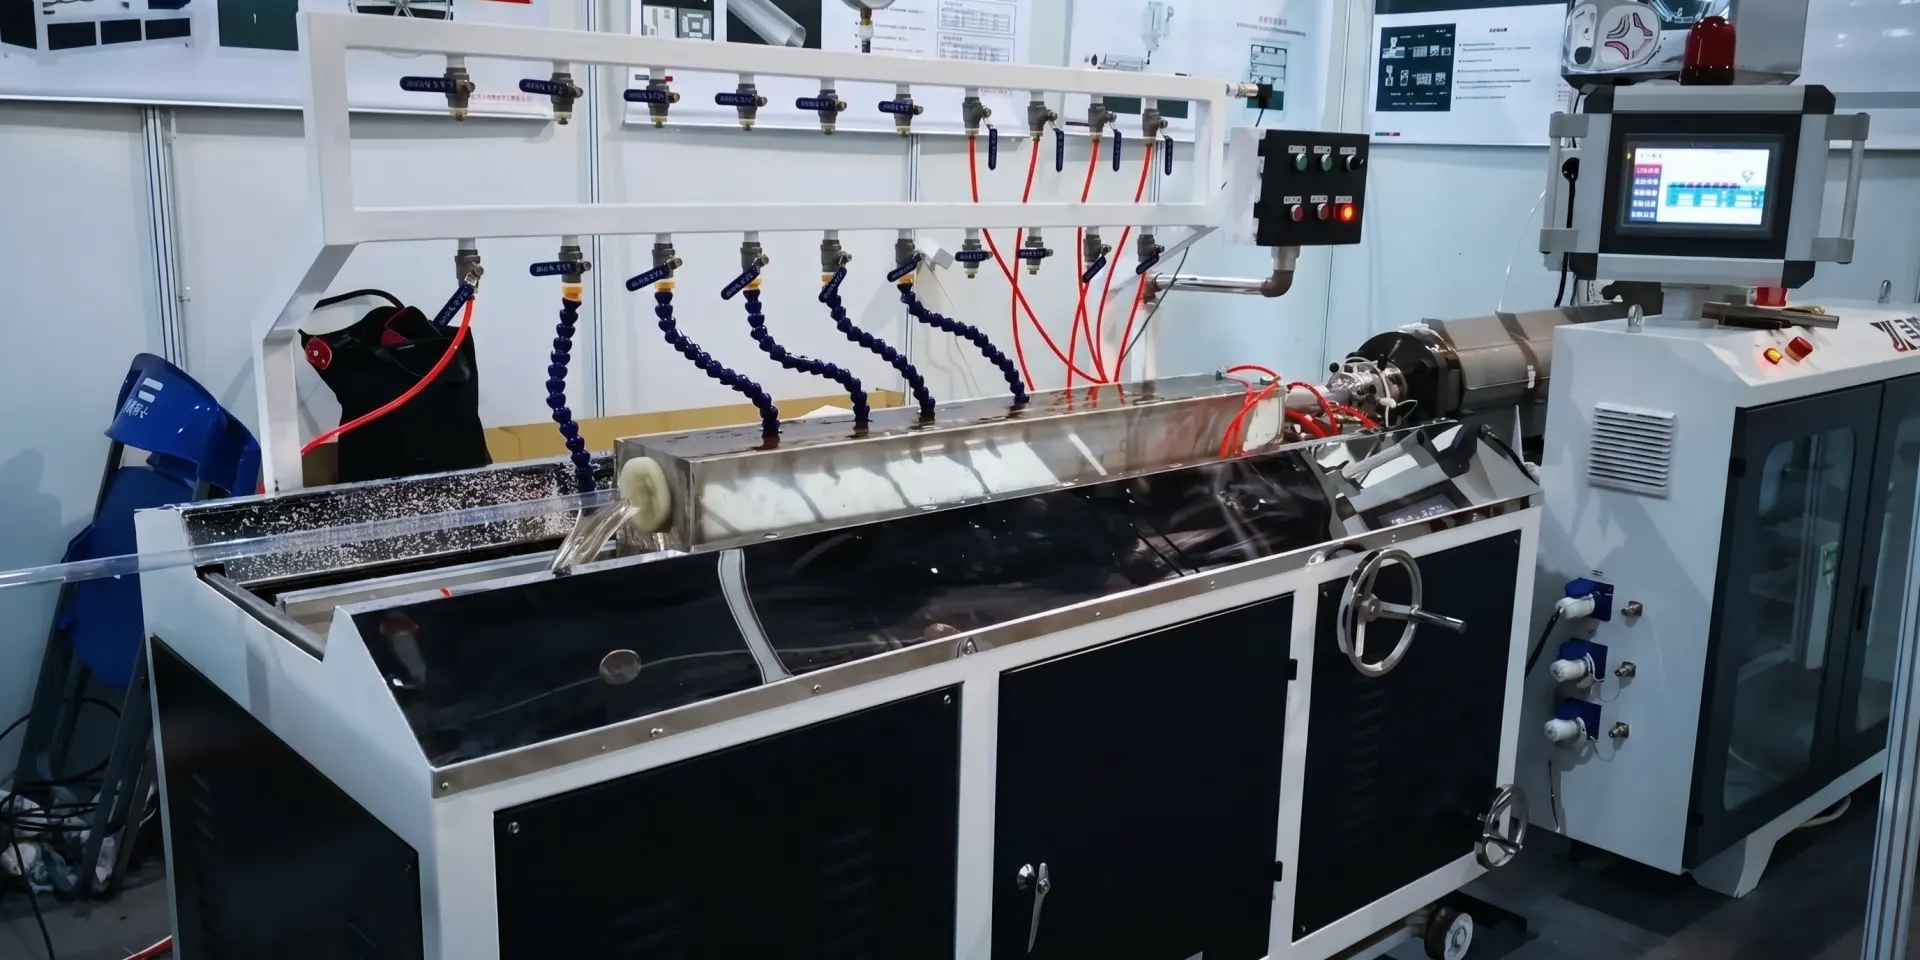
For a PU / TPU pneumatic tube project, material preparation, melt stability, OD / ID / wall control and collection method must be treated as one configuration. Hygroscopic grades require a verified drying route before extrusion; see resin drying in plastic extrusion for the roles of temperature, time, airflow and dew point. The confirmed tube tolerance then determines tooling, calibration, optional laser measurement and haul-off control, while the delivery format determines cutting or winding equipment.
Moisture and Bubbles
Some TPU / PU grades are sensitive to moisture. Residual moisture can create bubbles, surface defects or unstable extrusion. For moisture-sensitive projects, drying and stable material handling should be reviewed before confirming the line.
Temperature Stability
PU / TPU tube extrusion needs steady melt temperature and controlled shear. Overheating, unstable screw speed or a poorly matched die can create die lines, surface roughness or unstable tube dimensions.
Surface Marks and Drag
Flexible TPU can show drag marks when downstream contact is too aggressive. Calibration surface, water cooling, haul-off contact and guide alignment should be matched to tube hardness and surface requirement.
OD Control and Shrinkage
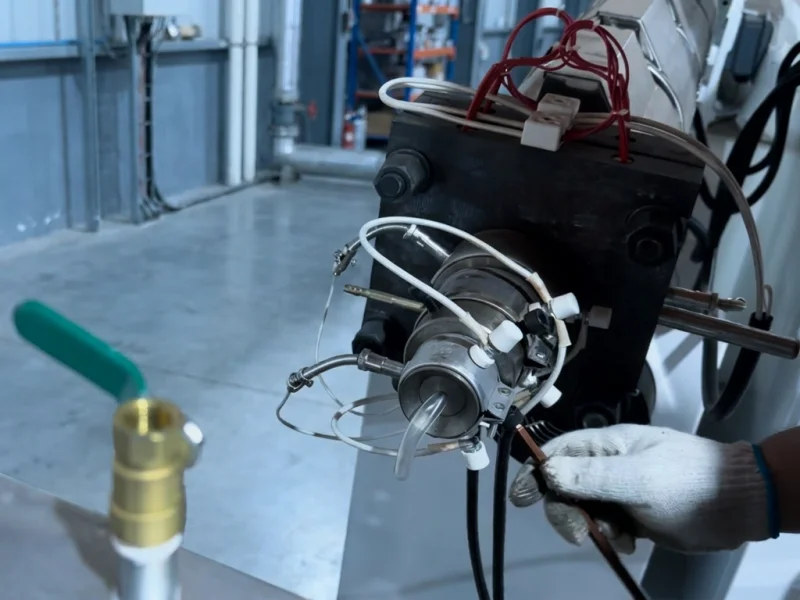
Dimensional stability depends on die matching, cooling consistency and haul-off synchronization. For tighter OD control or continuous production records, online laser diameter measurement can be added as an optional configuration.
Cutting vs Winding Tension
Soft flexible tubing can deform if downstream tension is too high. For coiled PU air tube, winding tension and reel handling matter as much as extrusion stability. For cut tube, cutter speed and tube support must be matched to line speed and hardness.