Jinxin supplies the complete configured dip tube extrusion line, not finished tubes. The configuration is matched to your PE (incl. LDPE) or PP tube sample and pump or valve connection.
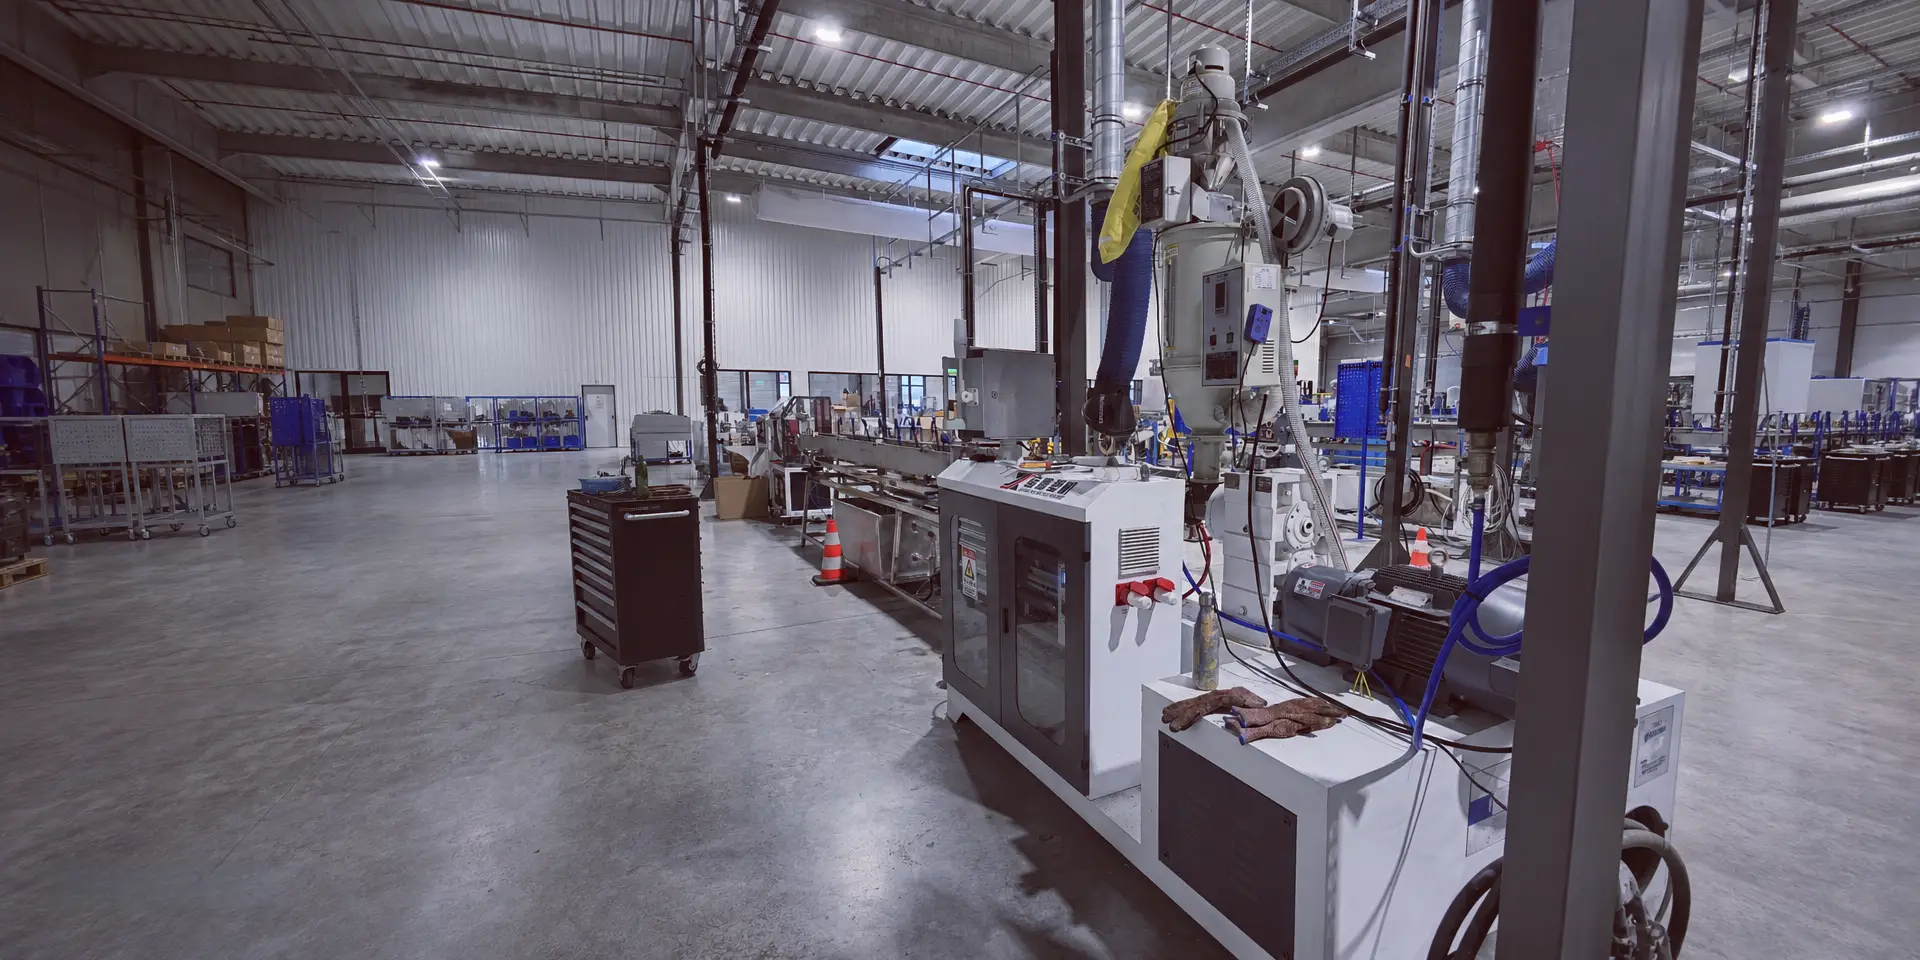
Dip tube extrusion line manufacturer
Dip Tube Extrusion Line
A factory-tested PE / PP dip tube extrusion line for aerosol valve, lotion pump, perfume pump and trigger sprayer packaging.
Quick Facts
Field Reference
Finished tube use Aerosol valve, lotion pump, perfume pump, trigger sprayer
Materials PE (incl. LDPE) / PP according to application
Typical OD range 3-10mm typical application range, confirmed by tooling and finished tube sample
OD stability target +/-0.05mm after configuration and test run
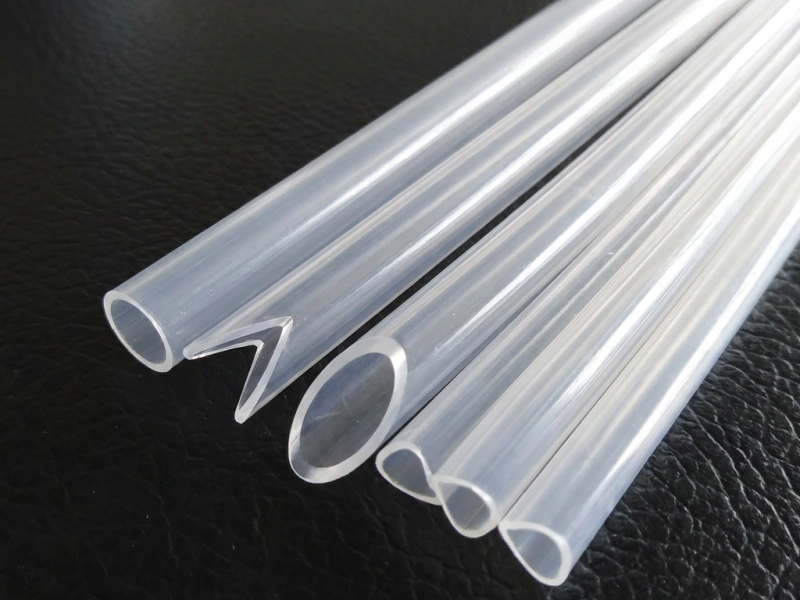
Cut-end profile Flat (square) cut / V-notch (custom angle) / slanted cut / concave cut - formed in-line by the servo cutter, no secondary trimming. Each profile needs its own dedicated cutter head, specified before production.
Collection method Servo cutting, horizontal winding or dual-shaft winding
Optional measurement Laser or ultrasonic online diameter measurement, quoted when required
Line type Complete dip tube extrusion line, not a standalone extruder
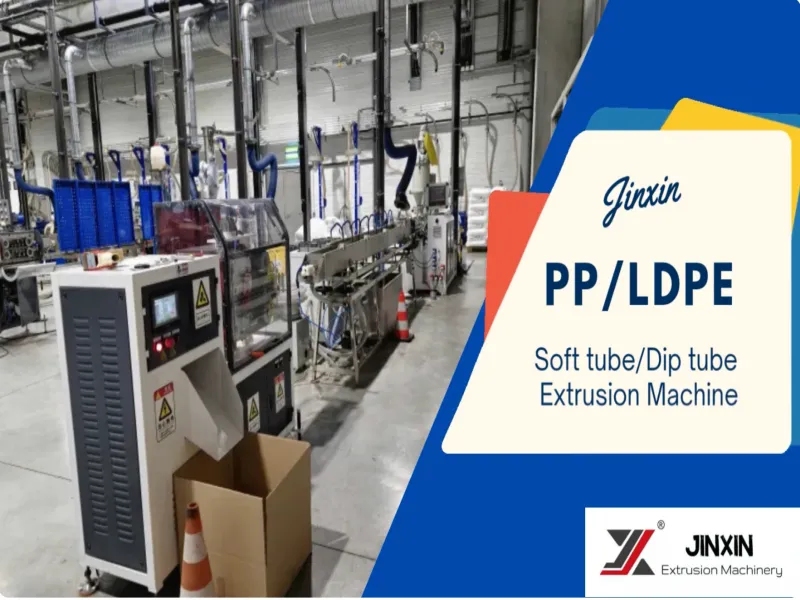
Dip Tube Line Running Video
Watch a Jinxin dip tube extrusion line running in real production. New configured lines are still verified against the agreed tube sample, material and cut requirement before shipment.
Roundness and outer diameter: Matched die tooling, vacuum calibration, stable cooling and synchronized haul-off control tube shape and dimensions.
Dry tube, stable pulling: Air-blow drying removes surface water after the cooling tank to reduce slipping at the haul-off.
Inner fit check: Smooth stainless-steel pin gauges check the tube's inner diameter and fit; they do not replace outer-diameter and roundness checks.
Watch Dip Tube Line RunningCompleted project record
What Jinxin Built and Verified
For a completed dip tube extrusion line project, Jinxin delivered on-site installation and commissioning. The line combined vacuum calibration, stable cooling, 360° air-blow drying, synchronized haul-off, online end cutting and pin-gauge fit verification to control tube dimensions and fitting consistency.
In-Line Cut-End Profiles
Jinxin's servo flying-knife forms the final end profile during extrusion: flat (square) cut, V-notch (custom angle), slanted cut or concave cut. No separate notching machine or secondary trimming step is needed for the specified profile.
Each profile is produced by its own dedicated cutter head, built to the buyer's specification. The V-notch angle is customizable. The required cut shape, V-angle and tube length must be confirmed before production and cannot be changed after the cutter head is made; additional profiles need additional heads, which can be quoted together.
Output Reference
Reference extrusion output: SJ35 is typically quoted around 8-10 kg/h, and SJ45 around 15-18 kg/h.
Line speed is calculated from tube gram weight, so the same kg/h output can convert to very different m/min or pcs/min. Jinxin calculates practical speed from the buyer's tube OD, ID, wall thickness, material density, cut length and collection method.
Recent sample reference: On SJ45 configurations, thicker LDPE dip tubes may convert to about 20 m/min, while lighter thin-wall PP dip tubes may calculate above 70 m/min. Final speed is confirmed after sample review and factory testing.
Output note: kg/h is the extrusion capacity; m/min is line speed; pcs/min also depends on cut length.
What's Included In The Dip Tube Line
From pellets to cut or wound tubes, the complete line is configured around your sample and output target. The table below shows the scope; detailed equipment specifications follow.
| Process Stage | Included Function |
|---|---|
| Extrusion and forming | SJ35 / SJ45 single screw platform, die head and tooling matched to the tube sample |
| Sizing and cooling | Vacuum calibration, cooling path and optional chiller support when required |
| Drying and pulling | 360 degree air-blow drying and synchronized haul-off |
| Collection | Servo cutting, horizontal winding or dual-shaft winding according to the buyer's production flow |
| Verification | Sample-based line verification before shipment |
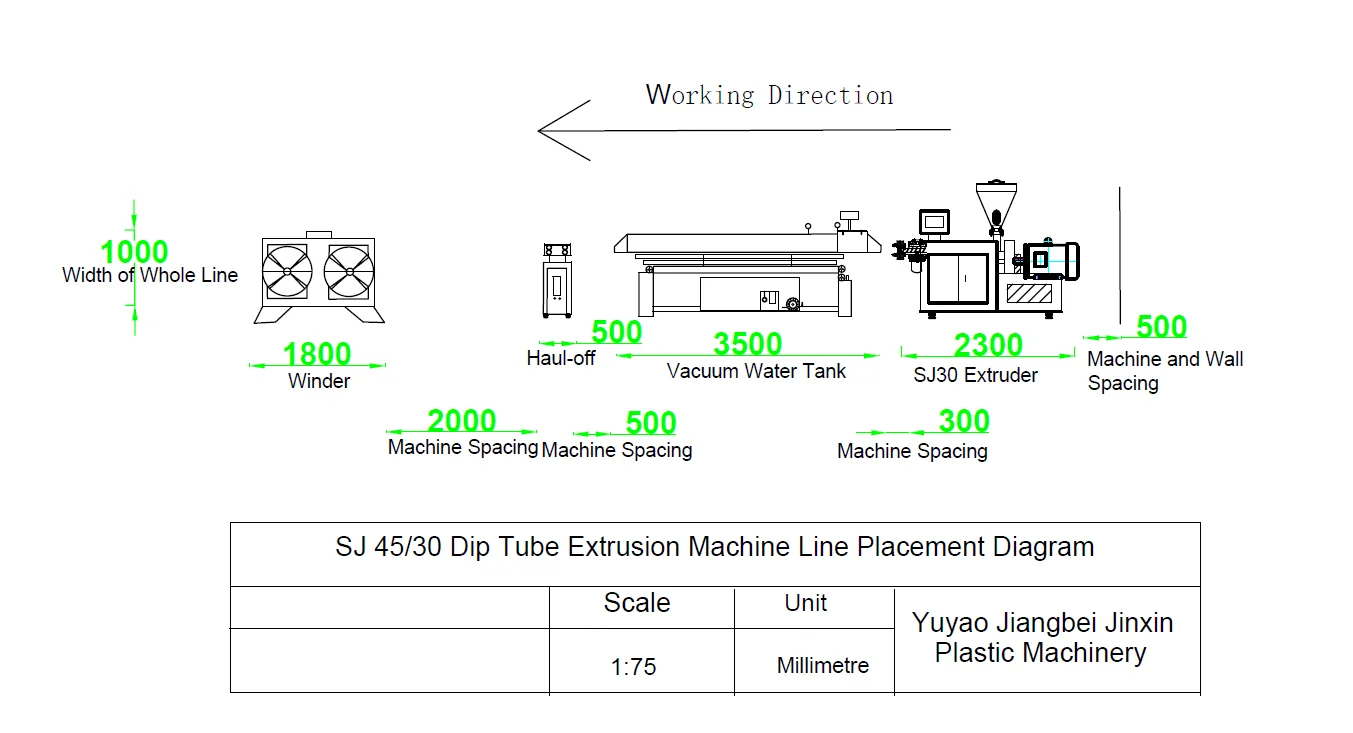
FOB turnkey reference range
Dip Tube Extrusion Line Price Range
FOB turnkey reference: USD 38,000-55,000 for a complete PE (incl. LDPE) / PP dip tube extrusion line.
This is a reference range for a configured turnkey line, not a bare-machine teaser price. The final quotation depends on the buyer's product sample, OD range, material, tolerance target, cut-end profile, collection method, line speed, optional online measurement, electrical standard, service scope and destination port.
Optional items that affect price
| Optional Item | When It Matters |
|---|---|
| Laser or ultrasonic online diameter measurement | For continuous OD monitoring, tighter QC records or higher automation |
| Custom cutter head | For flat (square) cut, V-notch (custom angle), slanted cut or concave cut geometry |
| Dual-shaft winder | For more continuous collection and smoother reel handling |
| Extra tooling sets | For additional OD or wall-thickness ranges beyond the confirmed quote |
| On-site installation | Quoted separately by destination and service days |
Final quote depends on sample, OD range, material, tolerance target, cut-end profile, collection method, line speed, optional measurement, service scope and destination port.
Send specs for exact FOB quoteComplete Dip Tube Production Line Modules
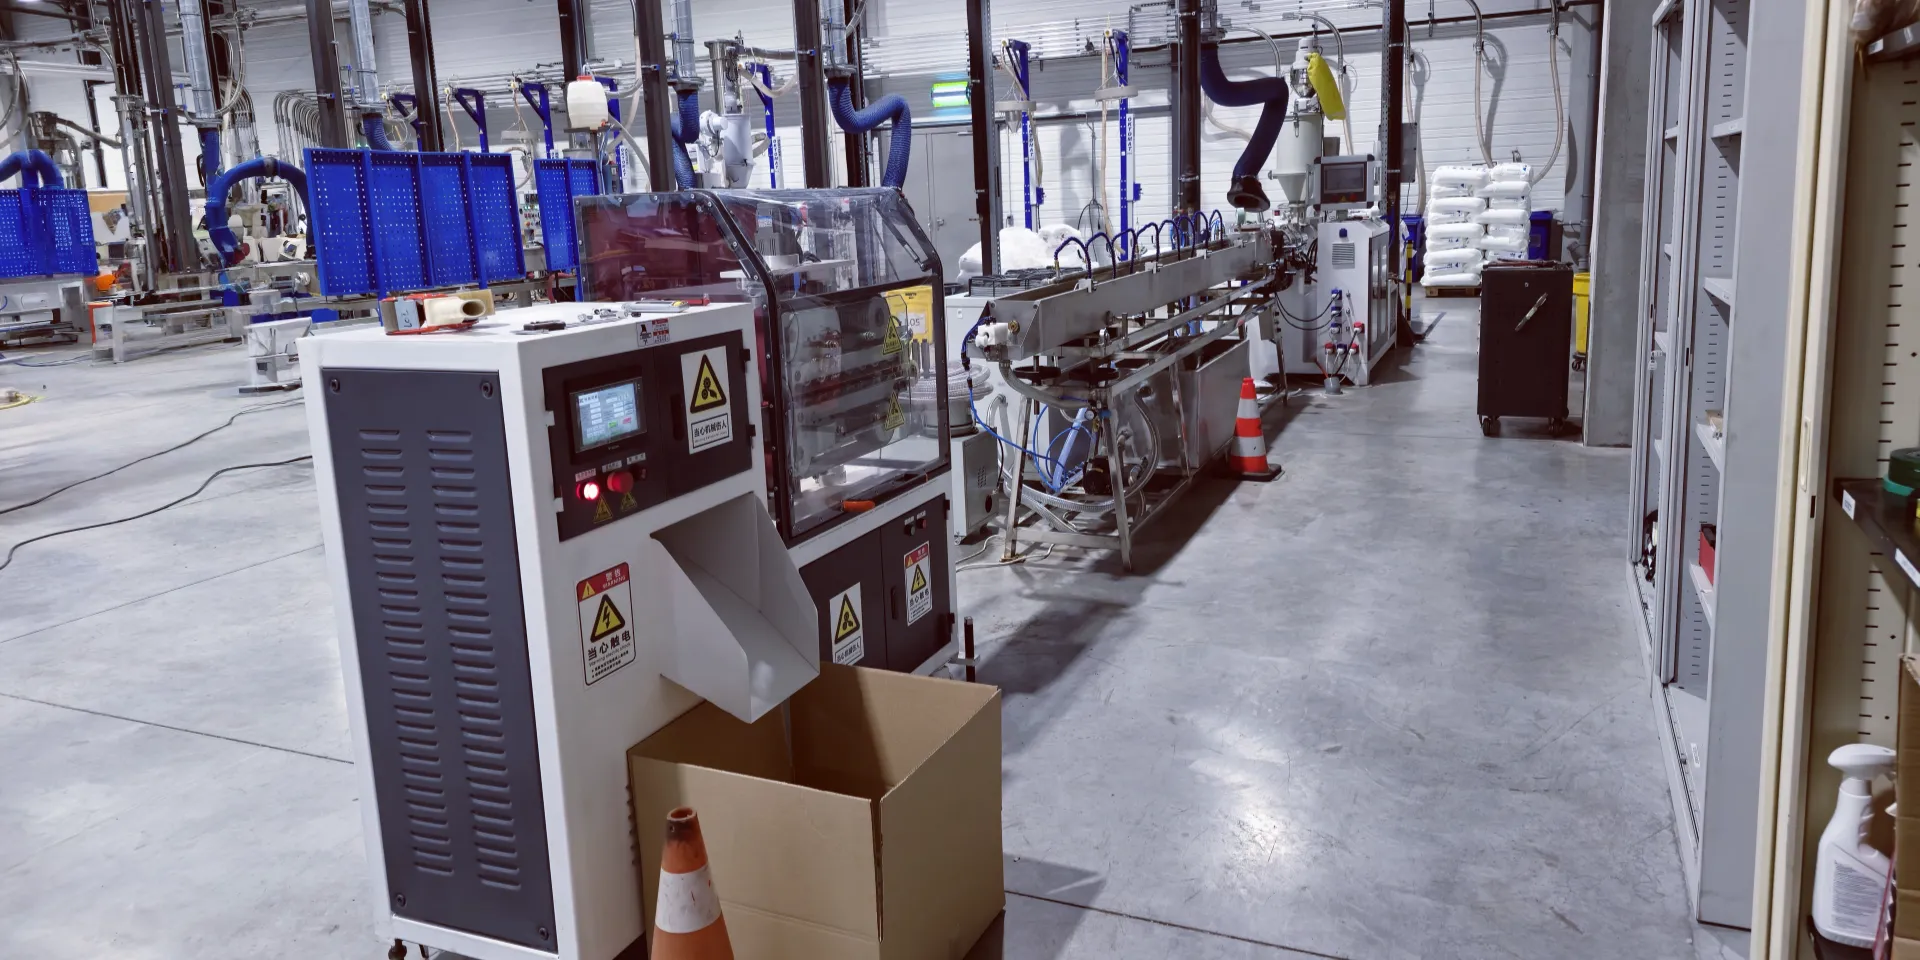

Main extrusion module
Precision Single Screw Extruder
The single screw extruder plasticizes PE (incl. LDPE) or PP pellets and delivers stable melt flow to the die head. For typical 3-10mm dip tube production, Jinxin configures SJ35 or SJ45 platforms so the screw output, melt residence time and temperature control match stable PE / PP small-tube production.
| Detail | Reference |
|---|---|
| Motor | Siemens Beide inverter-duty motor. |
| Drive | Direct coupling design without belt transmission. |
| Inverter | ABB ACS580 for stable speed control. |
| Control | WECON PLC and touchscreen interface. |
| Screw | Nitrided steel screw configured for PE (incl. LDPE) / PP melt stability. |
| Heating | Multi-zone temperature control with SSR control. |

Tube forming tooling
Die Head And Tooling Set
The die head forms the thin-wall tube and must match the target OD, wall thickness and drawdown behavior. Tooling is configured for the buyer's sample rather than copied from a generic tube size.
| Function | Why It Matters |
|---|---|
| Polished flow channel | Helps reduce melt stress and tube instability. |
| Matched core and sleeve | Controls OD, ID and wall thickness. |
| In-house adjustment | Allows correction during factory testing before shipment. |
| Size-specific tooling | Supports different tube sizes through matched tooling sets. |

OD calibration
Vacuum Calibration And Cooling Tank
The vacuum tank stabilizes tube roundness and OD while the tube cools. For dip tubes, this is one of the main controls behind assembly fit and leakage prevention.
| Detail | Reference |
|---|---|
| Construction | SUS304 stainless steel tank. |
| Alignment | 3-axis adjustment for die-to-haul-off centering. |
| Vacuum | Water-pump vacuum system for stable negative pressure. |
| Tube path | Integrated pressure rollers help keep the tube immersed. |
| OD control | Supports +/-0.05mm OD stability target after configuration. |

Surface drying
Integrated air-blow drying
The 360-degree air-blow channel removes surface water before haul-off and cutting. This reduces traction slip and helps keep cut length and OD stability more consistent.
| Function | Benefit |
|---|---|
| 360 degree air wiping | Removes water around the tube surface. |
| Drier haul-off contact | Reduces micro-slippage in pulling rollers. |
| More stable cutting | Helps improve cut length repeatability. |
| Cleaner collection | Reduces residual water before winding or packing. |

Synchronized pulling
Precision Haul-Off Options
The haul-off system synchronizes tube pulling with extrusion output. For typical 3-10mm thin-wall dip tubes, Jinxin usually configures a compact roller-type haul-off because the tube is small, light and does not require high pulling force. A precisely adjustable roller haul-off gives stable traction with a compact footprint. The key is fine roller gap and pressure control: too much pressure can mark or deform a thin tube, while too little pressure can cause slip, runout or length variation. Belt-type haul-off can be quoted when the tube material, softness or tolerance target requires a different pulling method.
| Option | Best For |
|---|---|
| Adjustable roller haul-off | Typical 3-10mm thin-wall dip tubes, compact layout and stable pulling. |
| Fine roller gap / pressure control | Reduces slip, tube marking and deformation risk. |
| Belt-type haul-off | Quoted when tube softness, wall thickness or tolerance target requires it. |
| Synchronized speed control | Supports stable OD and repeatable cut length. |

Cutting system
Delta Servo Cutting System
The servo flying-knife cuts each dip tube to length and forms the final end profile in-line. The cutter head can be customized to the required shape - flat (square), V-notch, slanted or concave.
| Detail | Reference |
|---|---|
| Drive | Delta servo motor and driver. |
| Length control | Encoder-based repeatable cutting. |
| Cut profiles | Flat (square) cut, V-notch (custom angle), slanted cut or concave cut. |
| Interface | Touchscreen settings for length, counting and alarm. |
| Custom head | Quoted according to required cut geometry. |

Tube collection
Horizontal Or Dual-Shaft Winder
Some dip tube production uses winding before later cutting or assembly. Jinxin configures the winding system according to tube softness, reel size and production flow.
| Option | Purpose |
|---|---|
| Horizontal winder | Gentler collection for fine or soft tubes. |
| Dual-shaft winder | More continuous winding for standard production. |
| Magnetic powder clutch | Supports steady winding tension. |
| Traversing unit | Keeps tube layers neat on the reel. |
| Custom reel setup | Matched to packaging or downstream handling. |
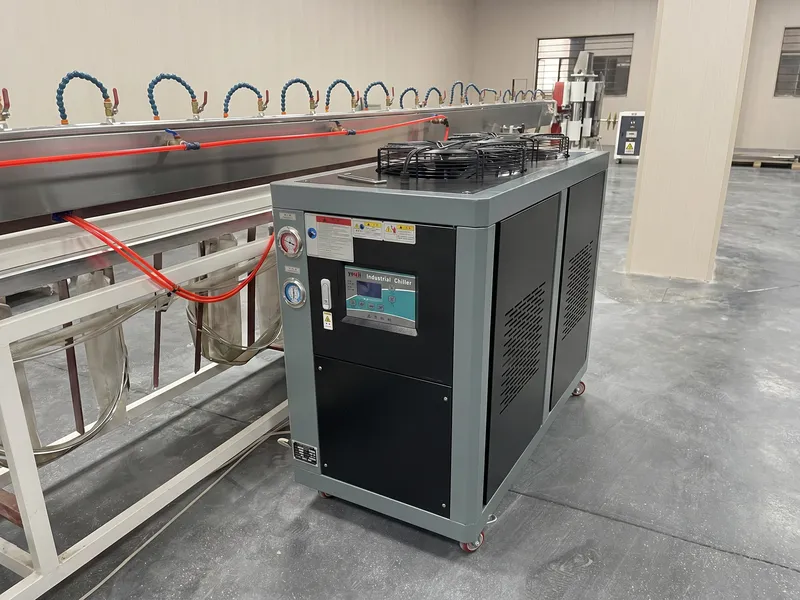
Cooling water support
Industrial Water Chiller
Stable cooling water helps keep the calibration process consistent during continuous production. The chiller reduces dependence on unstable civil water temperature.
| Item | Reference |
|---|---|
| Type | Air-cooled or water-cooled unit according to factory conditions. |
| Role | Supports stable calibration and cooling temperature. |
| Benefit | Helps reduce OD drift caused by water temperature changes. |
Applications

Lotion Pump Dip Tube Production
Lotion pump dip tubes need a stable interference fit inside the pump housing. LDPE is commonly used because it can bend inside the bottle while still holding shape during automated insertion.

Perfume Pump Dip Tube Production
Perfume pump tubes are often narrow and thin-wall. They need clean cut ends, stable OD and sometimes V-notch or slanted cuts to match fine mist sprayer geometry.

Aerosol Valve Dip Tube Extrusion
Aerosol valve dip tubes often use PE or PP depending on stiffness, chemical resistance and valve design. Stable roundness and material consistency help the tube fit reliably in pressurized packaging.

Trigger Sprayer Dip Tube Production
Trigger sprayer dip tubes for household and garden bottles may use larger diameters and wider tolerance windows than cosmetic pump tubes. Stable drying, haul-off and cutting still matter because surface moisture can cause traction slip and length variation.
Why Manufacturers And Procurement Leaders Choose Jinxin
01
Product-Based Factory Testing
Jinxin test-runs the agreed product type before shipment instead of only testing the machine empty. The goal is to confirm that the die, calibration, haul-off, cutting or winding system can produce the buyer's target dip tube under real extrusion conditions.
- Dimensional verification: Confirms OD, wall thickness and cut-end profile against the agreed sample.
- Startup reference data: Gives operators practical baseline settings after installation.
- Material calibration: Helps reduce startup guesswork when the buyer sends actual pellets.
- Test-run video: Provides visible proof before shipping.
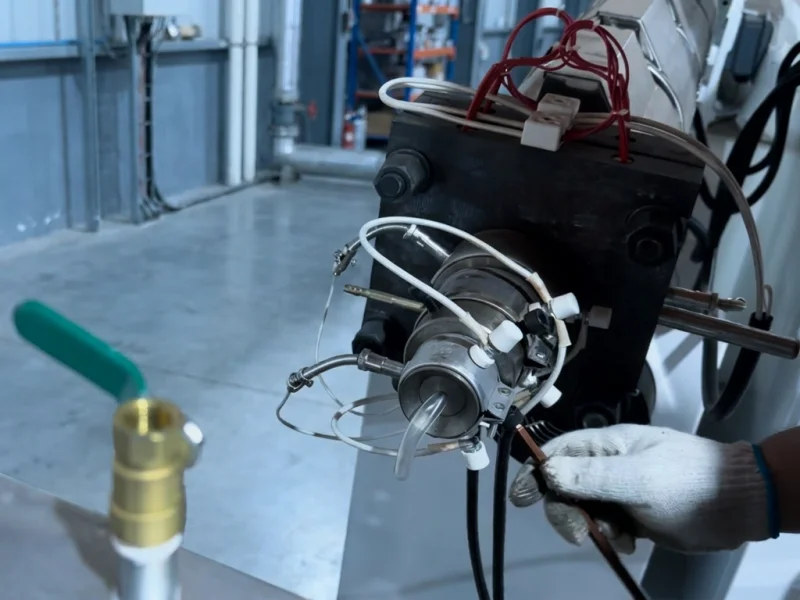
02
Transparent Line-By-Line Quoting
Jinxin quotes by configuration, not by a vague machine title. The quotation lists the extruder, tooling, tanks, haul-off, cutter or winder, chiller, control system, component brands, optional items and service scope.
- Equipment list: Makes the scope comparable with other suppliers.
- Component brands: Helps maintenance teams plan future replacement.
- Optional items: Separates laser/ultrasonic measurement, custom cutter head or extra tooling from the base line.
- Service items: Keeps installation and travel cost visible.
03
Global-Service Component Strategy
For core drives and controls, Jinxin uses industrial components selected for practical maintenance in overseas factories.
- Motor and drive: Siemens Beide and ABB are used according to configuration.
- PLC and HMI: WECON is used for practical line operation.
- Servo system: Delta servo system supports repeatable cutting.
Component brands: Siemens Beide, ABB, WECON, CHINT, Delta
Trust Credentials
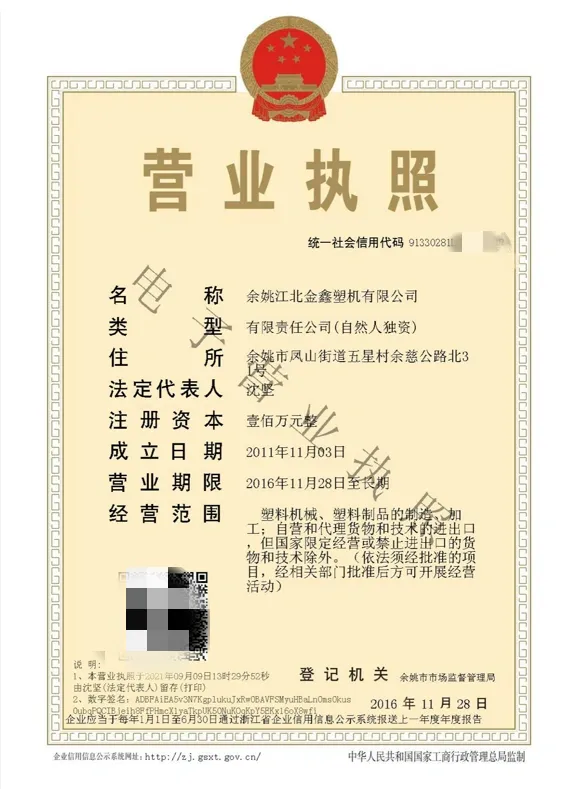
Jinxin Extruder is the manufacturing brand of Yuyao Jiangbei Jinxin Plastic Machinery Co., Ltd., a Ningbo-based extrusion equipment factory focused on configured single screw production lines. For dip tube projects, line configuration, factory testing, startup references and after-sales support are handled by Jinxin's factory team.
Manufacturing entity
Yuyao Jiangbei Jinxin Plastic Machinery Co., Ltd.
Brand
Jinxin Extruder
Founded
2012, Ningbo, Zhejiang, China
Focus
Single screw extrusion lines — no twin screw, no used equipment
Factory role
Direct project communication, line configuration, factory testing and after-sales support are handled by Jinxin's factory team
Export reach
15+ countries across Asia, Europe, Africa, and the Americas
Export support
Export packing and shipment documentation support after project confirmation
Founder credential
Nationally certified Electrician Operation Certificate
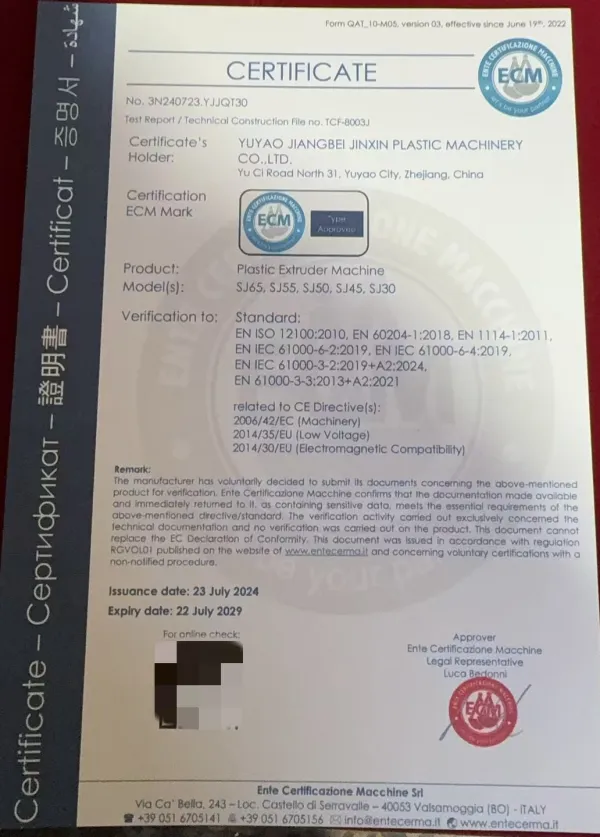
CE documentation for the main extruder
CE documentation is available for Jinxin main extruder models SJ30, SJ45, SJ50, SJ55 and SJ65 and is valid until 2029-07-22.
FAQ
FAQ - Dip Tube Extrusion Line
01 PE (including LDPE) or PP - which material should a dip tube extrusion line process?
PE, especially LDPE, is common for lotion pump, perfume pump and many cosmetic dip tubes because it provides flexibility inside the bottle. PP is used when higher stiffness or chemical resistance is needed, such as some aerosol valve tube applications. Jinxin confirms the screw, temperature profile and tooling according to the buyer's material.
02 Is 3-10mm OD enough for my project, or what if I need 2mm or 12mm?
3-10mm covers most cosmetic pump, perfume pump, trigger sprayer and aerosol valve dip tubes - it is a typical application range, not the mechanical limit of the extruder. Within this range, changing tube OD requires a matching die tooling set (die and core) and calibration sleeve.
For diameters outside this range - finer tubes around 2mm or larger tubes around 12mm - Jinxin reviews the target size against tooling, cooling and haul-off capability. Smaller tubes are more sensitive to cooling stability and haul-off alignment. Send a sample or drawing and Jinxin can confirm feasibility and configuration.
03 Some suppliers advertise 300 m/min dip tube lines - is faster better for my project?
For dip tubes, no. A headline like "300 m/min" is line speed, not output. A thin dip tube weighs very little per meter, so high line speed mainly adds cooling-tank length, footprint and energy use, not tube quality. Those lines are built for one tube size in huge volumes. For multi-size cosmetic, perfume, pump and aerosol dip tubes, +/-0.05mm OD precision, clean cut ends and fast changeover matter far more than peak m/min.
04 Is laser or ultrasonic online measurement standard?
No. Laser or ultrasonic online diameter measurement is optional. It can be added when the buyer needs continuous OD monitoring, tighter QC records, higher automation or traceability. Standard OD control relies on die matching, vacuum calibration, stable cooling, synchronized haul-off and factory test-run verification.
05 Do I need a separate dip tube cutting machine for V-notch or slanted ends?
No. The Jinxin line cuts the end profile in-line during production - flat (square) cut, V-notch (custom angle), slanted cut or concave cut - with no secondary trimming. The buyer specifies the profile and V-angle in advance; Jinxin builds the matching cutter head and verifies it on your material during the pre-shipment trial.
06 Can one line cut several end profiles, or change the profile later?
Each profile - flat (square) cut, V-notch (custom angle), slanted cut or concave cut - is formed by a dedicated cutter head built to your specification. The shape and V-angle must be confirmed before production and cannot be changed after the head is made; additional profiles need additional heads, which can be quoted together. The servo flying-knife then cuts that profile to length in-line, without stopping the line.
07 How do you ensure the dip tubes fit valves and pumps without falling off?
Jinxin controls outer diameter and roundness through matched die tooling, vacuum calibration, stable cooling and synchronized haul-off. Because a small soft tube can deform under caliper jaws, the factory test also uses a smooth graduated stainless-steel pin gauge set to check the inner fit: the selected pin is inserted into the tube to confirm whether the fit matches the agreed specification.
The pin-gauge check verifies inner diameter and assembly fit; it does not replace OD and roundness checks. If the buyer can send the actual valve or pump component, Jinxin can also perform a direct test-fit against that component.
08 Can one line cover multiple applications, tube sizes and small batches? What do I change when switching?
Yes. Lotion pump, perfume pump, aerosol valve and trigger sprayer dip tubes share the same extruder platform - the differences are in tooling, cut-end profile and collection method.
To be specific about what changes: switching tube OD requires changing the die and core (each OD has its own tooling set), along with the matching calibration sleeve. Vacuum and haul-off synchronization are reset, but the main extruder does not change. The practical approach for multi-size production is to have a tooling set for each commonly used OD, then swap tooling between runs rather than locking the line to one fixed size.
The quotation should be based on the buyer's actual tube family - how many ODs, which cut-end profiles, which collection method - not a generic high-speed catalog model.
09 What is the lead time, warranty and packing for ocean freight?
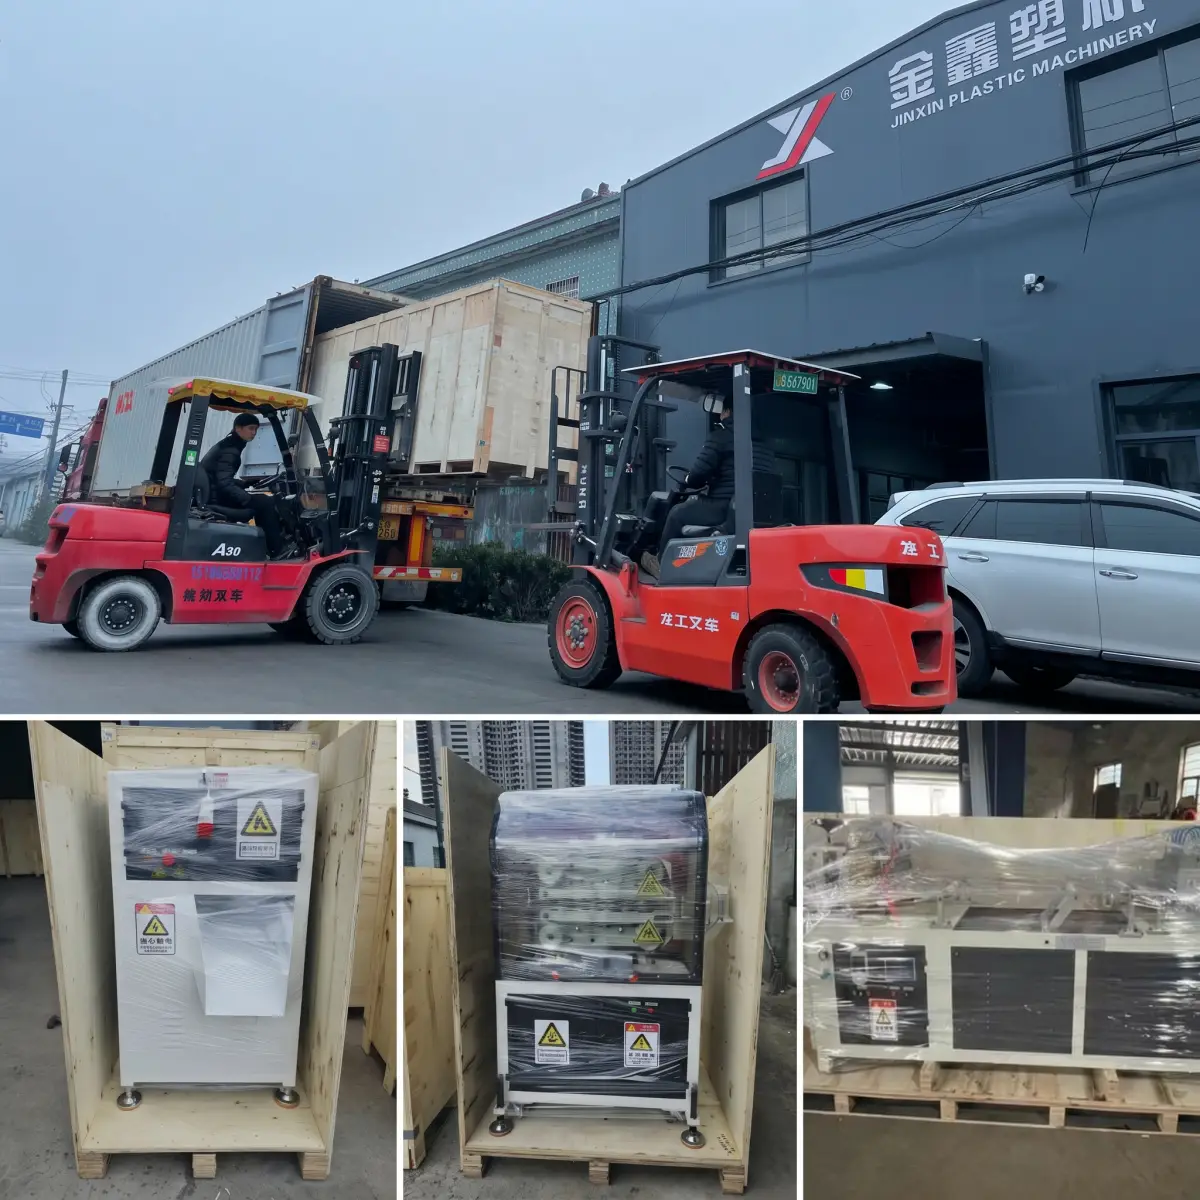
Lead time is confirmed according to configuration, tooling, electrical setup and factory test-run requirement. Many standard dip tube line projects are commonly planned around 50-60 working days from deposit. Warranty is quoted by full-line scope and component terms. Packing uses fumigation-free wooden crates, anti-rust protection and moisture-proof film, with larger stainless-steel tanks packed separately when required.
Dip tube extrusion line quote
Request My Dip Tube Line Quotation
Tell us what you want to make, even if you do not have every specification yet. Jinxin will help confirm the tube requirements and prepare an itemized FOB quotation for the complete line. Only your email is required to start.
Optional details for an accurate quotation
- Application
- Lotion pump / perfume pump / aerosol valve / trigger sprayer
- Material
- PE (incl. LDPE) / PP
- Tube size
- OD, ID and wall thickness
- Cut-end profile
- Flat (square) cut / V-notch (custom angle) / slanted cut / concave cut
- Cut length
- Required tube length and tolerance
- Collection method
- Cutting / horizontal winding / dual-shaft winding
- Output target
- Practical capacity or line speed target
- QC requirement
- Standard test-run verification or optional online measurement
- Factory standard
- Voltage, frequency and available space
- Destination
- Country and port